How to Choose a Flow Indicator Sight Glass?

Choosing a flow indicator sight glass is a practical decision, not a simple catalogue search. The device must show movement clearly while surviving pressure, temperature, vibration, and chemical exposure. A useful selection begins with the process fluid. Water, steam, oil, and corrosive chemicals each demand different glass, gasket, and body materials.

Dr. Béla G. Lipták, a respected process-control author, is often credited with saying, “Instrumentation is the eyes and ears of a process.” That principle applies directly here. A flow indicator sight glass gives operators visual evidence, but only when its design matches the installation. Check the pipe size, connection type, pressure rating, temperature range, and expected flow direction. Consider whether a clear window is enough, or whether a rotor, flapper, drip tube, or illuminated design is more suitable. Small details matter. A poorly positioned unit may show turbulence instead of stable flow.

Reliable selection also includes maintenance access and replacement planning. Ask how easily the glass can be inspected, cleaned, and changed. Confirm gasket compatibility and verify the manufacturer’s test documentation. Standards and site requirements should guide the final choice, not replace engineering judgment. This guide cannot predict every plant condition. Real systems are rarely perfect. Even an expensive flow indicator sight glass can mislead when air pockets, low flow, or dirty glass affect visibility. Careful observation remains essential. The right product makes flow easier to understand, safer to monitor, and more dependable during daily operation.
How to Choose a Flow Indicator Sight Glass?

Define the Process Duty: Fluid, Temperature, Pressure, and Flow Range

Choosing a flow indicator sight glass starts with the process duty, not the pipe size.

Identify fluid composition, temperature, pressure, and flow range before reviewing designs.

A clear liquid may need a simple window. Viscous oil or slurry may demand lighting, larger ports, or revised internal geometry.

Record normal and upset conditions. Both matter. Include density, viscosity, solids content, color, and corrosive behavior. These details affect visibility, sealing, and material selection.

Measure temperature at the glass location, rather than copying a general equipment datasheet.

Hot fluid can weaken seals and create thermal stress during startup. Pressure rating should cover operation, cleaning, shutdown, and pressure pulses.

Do not treat vacuum as zero pressure. It creates a separate design load.

A common mistake is selecting the sight glass for average pressure only. That assumption can cause poor viewing and premature maintenance.

Flow range determines whether movement will be visible.

Very low flow may appear stagnant through a standard window. High flow can create turbulence, splashing, or vibration.

  • Compare minimum, normal, and maximum rates.
  • Note whether the line runs continuously or intermittently.
  • Ask how operators will read it: direct sight, illuminated viewing, or a rotor and flapper.
  • Confirm orientation and drainage, because trapped fluid can distort observations.

If process data is uncertain, state that clearly and verify it onsite. A confident guess is still a guess.

Have a qualified engineer check materials, gasket compatibility, pressure class, and inspection access before approval.

Match Connection Size and Pressure Class with ASME B16.5 Ratings

How to Choose a Flow Indicator Sight Glass?

Match Connection Size and Pressure Class with ASME B16.5 Ratings

Choosing a flow indicator sight glass starts with the process line, not the window diameter. Confirm the pipe’s nominal size, flange facing, bolt pattern, and gasket type. ASME B16.5 establishes dimensions, pressure classes, and temperature ratings for flanges from NPS 1/2 through NPS 24. Its 2022 rating tables list carbon-steel Class 150 at approximately 285 psi at 100°F, while Class 300 reaches about 740 psi. These values change with temperature and material group.

Do not treat Class 300 as simply twice Class 150. At higher temperatures, allowable pressure decreases. The ASME B16.5 tables must be checked against the sight glass body material, flange material, and design temperature. A mismatch can appear harmless during installation, yet create leakage around a hot, vibrating line. The 2023 Global Energy Monitor pipeline data show thousands of new and existing industrial pipeline projects worldwide, highlighting why standardized connections remain important for maintenance and replacement planning.

Field experience also exposes a common oversight: the glass rating may differ from the metal body rating. Verify the manufacturer’s pressure-temperature curve, window material, bolt loading, and test pressure. ASME B16.5 does not qualify every sight glass assembly. It mainly defines the flange interface. Check the actual unit.

That detail is easy to miss.

Select Borosilicate Glass to DIN 7080 or DIN 28120 Requirements

How to Choose a Flow Indicator Sight Glass?

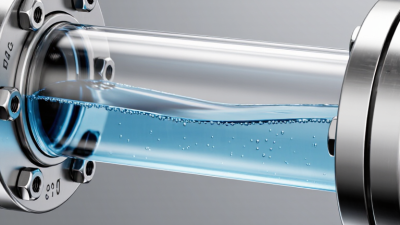
When selecting a flow indicator sight glass, begin with the applicable standard. DIN 7080 focuses on borosilicate glass used in sight glass assemblies. DIN 28120 addresses sight glass fittings for process equipment. The two requirements are related, but they are not interchangeable.

Check the glass dimensions, pressure rating, temperature range, and sealing arrangement against the equipment design. Borosilicate glass offers strong thermal resistance and good chemical durability. It also provides a clear view of liquid movement, bubbles, color changes, and suspended particles. Small details matter. Confirm whether the assembly needs a welded, bolted, or threaded connection. The fitting must match the pipe size and installation direction.

Process conditions should guide the final choice. Consider pressure spikes, rapid temperature changes, abrasive media, and cleaning chemicals. A gasket may be suitable for one fluid but unreliable for another. Ask for material certificates, dimensional drawings, pressure data, and inspection records. Do not rely on appearance alone. A polished glass window can still be unsuitable for the service.

A useful field lesson is to inspect the viewing area after installation, not only before it. Misalignment, overtightening, or trapped stress can create problems later. I have also found that visual clarity is sometimes prioritized too highly. Safety margins, traceability, and maintenance access deserve equal attention. Recheck the actual operating conditions before approving the specification.

Choose Drip, Rotor, or Flapper Indicators for the Required Flow Direction

How to Choose a Flow Indicator Sight Glass?

Selecting a flow indicator sight glass starts with the required flow direction. In field inspections, I have seen correct instruments installed backward, making a clear window nearly useless. Drip indicators suit downward flow, where liquid forms visible drops through a small passage. They work well for low or intermittent flow. Rotor indicators are often better for horizontal flow because the rotor responds to moving liquid across the viewing area. Flapper indicators suit one-way flow and provide an immediate visual signal when the stream lifts the internal flap. Always compare the arrow on the body with the actual pipe direction. A small mismatch can create misleading readings.

Tips: Check the pipe orientation, fluid clarity, expected flow range, and pressure before choosing. Confirm whether the indicator needs vertical mounting, horizontal mounting, or a specific straight-pipe length. A rotor may barely move at low flow. A flapper can remain open during unstable flow. These details matter.

Use the process fluid’s temperature and chemical properties to assess window, seal, and body materials. Clean water and viscous oil behave differently, even at similar flow rates. For gas service, a liquid-style drip indicator may be unsuitable. I would also inspect the sight glass during commissioning, not only during purchase. The first reading may expose vibration, trapped air, or an installation error. That check is easy to skip. It should not be.

How to Choose a Flow Indicator Sight Glass? - Choose Drip, Rotor, or Flapper Indicators for the Required Flow Direction

Selection Dimension Drip Indicator Rotor Indicator Flapper Indicator
Operating principle Liquid passes over a small viewing chamber or drip plate, allowing the observer to see individual drops or an intermittent stream. A rotor, wheel, or impeller turns when fluid passes through the viewing chamber. Rotation provides a visual indication of flow. A hinged flapper, paddle, or flag moves with the fluid stream. Its position indicates whether flow is present and, in some designs, its approximate direction.
Best indication type Visual flow confirmation
Especially useful for low-volume liquid discharge and drain lines.
Flow presenceRelative activity
Faster rotor movement generally indicates greater flow, but it is not a calibrated flow measurement.
Flow presenceDirection check
Useful where a clear moving/non-moving indication is required.
Preferred flow direction
Suitable media Clean, low-viscosity liquids that form visible drops or a narrow stream. Clean liquids and some gases, provided the rotor is correctly sized and the process conditions are suitable. Clean liquids and gases where the flapper can move freely without being blocked by solids or deposits.
Low-flow performance Good when the rotor has low friction and the flow is sufficient to start rotation. Good for basic flow/no-flow checks, but very low flow may not move the flapper reliably.
Direction verification Limited. The visual stream normally confirms flow through the viewing path but may not clearly identify reverse flow. Limited to moderate. Rotor movement confirms flow; direction depends on the rotor geometry and viewing design.
Relative flow indication Low. Drop frequency can suggest changes, but it is not a reliable quantitative indication. Low to moderate. Flapper angle or movement can show activity, but it should not be treated as a calibrated reading.
Pressure-drop tendency Generally low, depending on the internal passage and connection size. Low to moderate; the rotor and internal supports add resistance to the flow path. Low to moderate; the flapper and hinge can create resistance, particularly at higher flow rates.
Maintenance considerations Keep the viewing area clean and inspect for blockage, staining, or loss of visibility. Check for rotor fouling, bearing wear, deposits, and restricted movement. Check the hinge or pivot for sticking, deposits, corrosion, and mechanical damage.
Sensitivity to solids or viscous fluids Poor to moderate. Solids can obstruct the viewing path, while viscous fluids may not form clear drops. Moderate to poor. Solids or high viscosity can prevent reliable rotor movement. Moderate to poor. Solids can restrict the flapper, and high viscosity can slow its response.
Installation requirements Install in the specified orientation and provide adequate lighting and visibility around the viewing section. Follow the marked flow arrow, maintain the required orientation, and avoid excessive vibration where possible. Follow the flow arrow and orientation instructions; allow sufficient straight pipe and clearance for free flapper movement.
Typical applications Drain lines, seal-water discharge, condensate observation, sampling points, and low-volume liquid outlets. Cooling-water circuits, lubrication systems, process-water lines, and other applications requiring an easy visual flow trend. Pump discharge checks, cooling circuits, lubrication lines, gas-flow confirmation, and applications requiring clear flow-direction verification.
Primary advantages Simple visual confirmation, strong visibility at low liquid flow, and straightforward operation. Continuous moving indication, useful visual response to changing flow, and easy observation through the sight window. Clear flow/no-flow indication, good direction awareness, and a simple mechanical design.
Main limitations Not suitable for reliable quantitative measurement and generally less effective for gas service or unclear liquid streams. Rotor movement may be affected by viscosity, deposits, orientation, and flow pulsation; it is not a substitute for a calibrated flowmeter. Very low flow may not overcome hinge friction, and incorrect orientation can cause false or weak indications.
Recommended choice

Selection note: Confirm the process fluid, viscosity, temperature, pressure, connection size, materials of construction, installation orientation, and required flow direction before specifying a sight glass. These indicators provide visual confirmation and should not be used as calibrated flow measurement devices unless the specific design has been tested and certified for that purpose.

Verify Materials, Sealing, Visibility, and ISO 9001 Quality Records

How to Choose a Flow Indicator Sight Glass?

Verify Materials, Sealing, Visibility, and ISO 9001 Quality Records

Choosing a flow indicator sight glass starts with the process fluid, temperature, pressure, and cleaning method. Stainless steel wetted parts suit many corrosive services, but not every grade performs equally. Confirm compatibility using chemical-resistance data, not appearance. ASME B16.5 and DIN 28120 provide useful guidance for flanges, dimensions, and sight-glass construction. A small mismatch can become a costly leak.

Sealing deserves close inspection. Check gasket material, compression, bolt loading, and temperature limits. PTFE may resist chemicals well, while elastomers can offer better flexibility. The wrong seal fails quietly. Inspectors should also examine glass type, viewing diameter, illumination, and contrast. A clear window is not automatically a readable window. Condensation, scale, vibration, or poor lighting can hide weak flow. A short field trial under operating conditions often reveals defects that catalog photographs miss.

Quality records add another layer of confidence. The ISO Survey 2022 reported 1,265,216 ISO 9001 certificates across 189 countries, showing the broad use of documented quality systems. Certification alone proves little about one sight glass. Request material certificates, pressure-test results, gasket traceability, calibration records, inspection reports, and nonconformance history. Records should identify heat numbers and final inspectors. Missing paperwork is a warning. I would still question an incomplete file, even when the equipment looks flawless.

How to Choose a Flow Indicator Sight Glass

This practical evaluation model prioritizes material verification, sealing performance, visibility, and ISO 9001 quality records. Confirm the selected sight glass against the actual fluid, temperature, pressure, corrosion conditions, applicable drawings, and project specifications before purchase.