A 200*1800mm Graphite Electrode is a compact product, but its performance depends on more than diameter and length. In electric arc furnace operations, electrode conductivity, bulk density, oxidation resistance, and joint quality affect current transfer and service life. Small differences matter. A worn nipple or chipped end can interrupt a shift.
The World Steel Association reported global crude steel production of 1,882.6 million tonnes in 2024. This scale shows why reliable furnace consumables matter, but it does not measure demand for any specific electrode size. That distinction is important. Buyers comparing Chinese manufacturers should request current product specifications, inspection records, and test methods—not rely on catalog claims alone. Check actual dimensions, resistivity, flexural strength, and packaging details. Ask how each batch is traced.
A credible expert quotation needs a verifiable source. No interview or published statement from a named specialist on this exact size was supplied, so attributing a quotation here would create false authority. That is a limitation worth correcting before publication. For now, the practical question is clear: can a supplier show that its 200*1800mm Graphite Electrode matches the furnace’s operating conditions, batch after batch? A low price is easy to print. Consistency takes evidence.
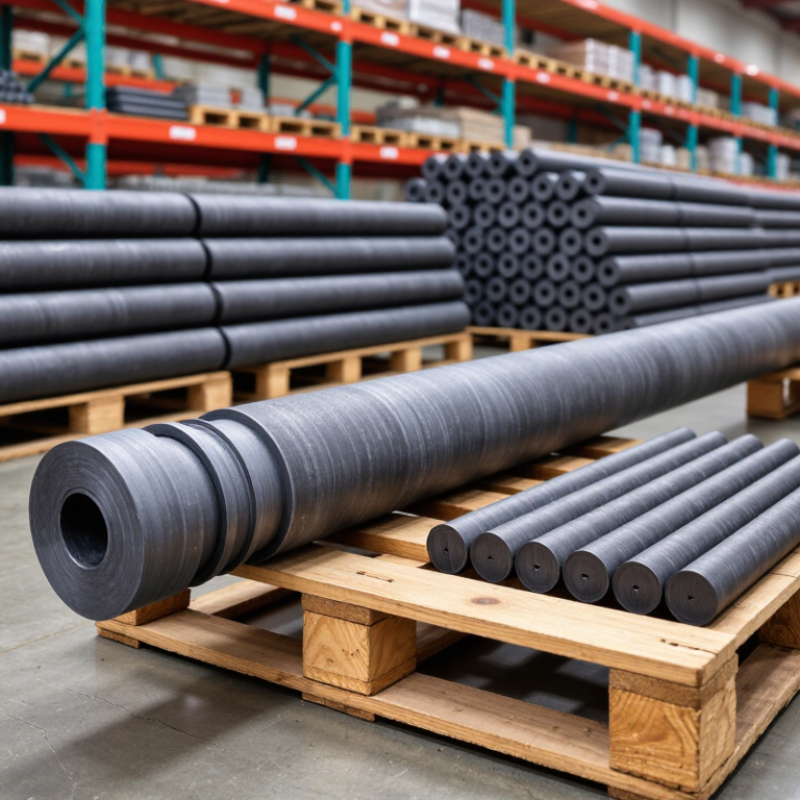
A 200 × 1,800 mm graphite electrode is a cylindrical conductor used in electric arc steelmaking. The first measurement usually refers to its nominal diameter; the second indicates its length. Confirm both against the product drawing, since measurement conventions can vary.
In the furnace, graphite conducts electrical current to create an arc that melts the metal charge. That is the basic function.
During operation, the electrode tip faces intense heat and repeated thermal stress. Sections are joined with threaded connectors as the working length is consumed.
A 200 mm diameter may suit certain furnace designs and power conditions, but size alone does not establish compatibility. The 1,800 mm length also affects handling and the available working column. Not by size alone.
Selection should account for furnace current, electrode quality, connection design, and operating practice. Operators may notice uneven wear, loose joints, or oxidation around exposed sections; each can affect consumption. Small details matter.
One easy mistake is treating nominal dimensions as a performance guarantee. Real furnace conditions are less tidy, and specifications should be checked alongside actual operating data.
A 200 × 1800 mm graphite electrode needs more than a matching size label. Check diameter, usable length, end-face condition, and straightness against the purchase drawing. Small errors matter. For a 200 mm diameter and 1.8 m length, the calculated volume is about 0.0565 m³. At a bulk density of 1.60–1.70 g/cm³, the estimated mass is roughly 90–96 kg, before machining details. These are indicative values, not a substitute for a grade-specific inspection certificate.
Bulk density and electrical resistivity help assess consistency, but grade and production route affect both. Technical datasheets commonly report density near 1.60–1.70 g/cm³ and resistivity around 7–10 μΩ·m for standard-grade electrodes; confirm the actual limits with the supplier. ASTM C559 describes bulk-density measurement for carbon and graphite, while ASTM C611 covers electrical resistivity testing. Use the stated test method when comparing results. The World Steel Association’s World Steel in Figures 2024 reports 1.89 billion tonnes of crude steel production in 2023, underscoring the scale of electrode use in steelmaking. A specification still cannot reveal every flaw. Inspect the delivered pieces and review batch test data; paperwork alone can feel reassuring, but it is not the whole check.
Typical indicative specifications for a 200 mm diameter × 1,800 mm long graphite electrode. Values vary by grade and production specification; confirm the applicable limits with the supplier before ordering.
| Specification | Unit | RP Grade — Typical Range | HP Grade — Typical Range |
|---|---|---|---|
| Nominal diameter | mm | 200 | 200 |
| Nominal length | mm | 1,800 | 1,800 |
| Bulk density | g/cm³ | 1.60–1.72 | 1.65–1.78 |
| Electrical resistivity | µΩ·m | 7.0–10.0 | 5.5–8.5 |
| Dimensional tolerance | — | Diameter and length tolerances are subject to the agreed product standard and purchase specification. | |
| Data basis | — | Indicative industry ranges, not guaranteed acceptance limits or a specific manufacturer's product data. | |
For a 200 × 1800 mm graphite electrode, current density helps relate electrical load to the electrode’s cross-sectional area. At 200 mm diameter, the area is about 314 cm². A density of 10–40 A/cm² therefore corresponds to roughly 3.1–12.6 kA. These figures are estimates, not operating instructions. Actual limits depend on furnace design, cooling, connection quality, and operating cycle.
RP grades are commonly used toward the lower end of the range, around 10–15 A/cm². HP grades may suit roughly 15–25 A/cm², while UHP grades can support higher densities, sometimes approaching 40 A/cm². Ranges overlap. A grade name alone cannot determine a safe load. Check the electrode’s technical data and confirm conditions with measured current, voltage, and connector temperature. Watch for hot spots near the nipple. Small differences in contact or furnace practice matter. The broad range is useful, but it can hide real operating limits.
Needle coke sets the foundation for a 200 × 1,800 mm graphite electrode. Incoming checks commonly cover particle size, moisture, sulfur, and thermal expansion. The coke is crushed, screened, blended with pitch, and extruded into a green cylinder. Baking then removes volatiles and strengthens the body; some production routes add pitch impregnation and rebaking. Small defects matter.
Graphitization heats the baked electrode to roughly 2,800–3,000°C, reorganizing carbon into a highly conductive structure. Temperature uniformity and furnace conditions affect resistivity and mechanical strength. After cooling, machining controls diameter, length, end-face flatness, and nipple-thread fit. Inspection should also record bulk density, electrical resistivity, and visible cracks, with results traceable to each production batch. A smooth surface alone proves little.
Demand makes consistency consequential. World Steel Association’s World Steel in Figures 2024 reports that electric-arc furnaces produced 28.6% of global crude steel in 2023. USGS Mineral Commodity Summaries 2025 estimates 2024 natural graphite mine production at 1.6 million tonnes; natural graphite is not needle coke, but the figure shows the scale of carbon-material supply. One uncomfortable point remains: even a well-controlled process can produce variation between batches, so inspection records and corrective feedback matter as much as a polished final surface.
For a 200×1800 mm graphite electrode, verify the drawing, tolerances, thread dimensions, and inspection method before comparing quotations. World Steel Association’s World Steel in Figures 2024 reports 1,892.2 million tonnes of crude steel production in 2023; electric-arc furnaces accounted for about 28.6%. This scale makes consistent electrode supply important, but it does not prove any single supplier’s capability. Ask for recent test records covering resistivity, bulk density, flexural strength, and dimensional checks. ASTM C611 and ASTM C1025 provide recognized methods for measuring electrical resistivity and modulus of rupture. A tidy certificate is not enough.
Traceability should connect each finished electrode to its raw-material batch, forming date, baking and graphitization records, machining inspection, and shipment documents. Request a sample batch record and check whether its identifiers match the product markings and packing list. During an audit, compare written procedures with actual shop-floor labels and measurement equipment. Small details matter. One weakness in this check is that polished documents can still hide inconsistent daily practice.
Capacity claims need similar scrutiny. Ask for monthly output specifically for the 200×1800 mm size, current lead time, planned maintenance, and recent on-time delivery performance. Confirm whether forming, baking, graphitization, and machining are controlled in-house or depend on outside suppliers. Review bottlenecks, not just total plant capacity: a large furnace may still leave machining as the limiting step. Capacity figures can be optimistic, so compare them with production schedules and shipment records.